

 EU
Choosing the wrong metal machining process is an expensive mistake. It shows up later as blown tolerances, poor surface finish, and metal parts that cost more than they should. The right choice depends on the workpiece material, geometry, tolerance, and volume in front of you.
This guide covers 13 main metal machining techniques, split into traditional machining processes and non-traditional methods, with what each one does best and how to pick the right one for your part.
What Is Metal Machining?

Metal machining is a subtractive manufacturing process that removes material from a solid workpiece until the part reaches its desired shape and finish. It starts from a solid block, bar, or casting of raw material. This makes it the opposite of 3D printing (additive manufacturing) and different from metal fabrication, which starts from sheet metal. It remains one of the most reliable manufacturing methods for complex metal parts and precision components.
Most metal machining today runs on CNC machines, where numerical control guides the tool for accuracy and repeatability. Advanced CNC machines achieve high precision across complex geometries. As a general benchmark, standard CNC machining holds about ±0.125 mm, precision machining reaches ±0.025 mm, and grinding or electrical discharge machining can hold ±0.0025 mm on critical features.
The main metal machining tools include lathes, milling machines, drills, and surface grinders. A versatile machining process like CNC milling scales from prototypes to mass production across metal alloys, brittle materials, and softer materials like plastics.
Metal Machining vs Metal Fabrication
Metal machining and metal fabrication solve different problems. Metal machining is subtractive. The material removal process cuts a solid block of raw material down to a finished part. Metal fabrication builds parts from sheet metal using techniques such as cutting, bending, and welding.
Metal machining suits complex, high-precision metal parts. Metal fabrication suits enclosures, frames, and large sheet metal assemblies. Metal machining is slower but more accurate. Metal fabrication is faster for sheet-based work. Many projects use both, with metal fabrication forming the structure and metal machining finishing the precise features. The choice comes down to geometry, raw material, and required tight tolerances.
Main Types of Metal Machining Processes
Machining techniques fall into two categories, and knowing which one a job needs is the first step in material selection and process planning.
Conventional machining uses a physical cutting tool that contacts the workpiece and shears away excess material to reach the desired shape. Turning, milling, and drilling are conventional metal cutting operations. These cover most everyday parts and are faster and cheaper for standard shapes.
Non-conventional machining removes material without a traditional cutting tool, using thermal, electrical, or abrasive energy instead. Machinists use these techniques when the stock is too hard, the feature too intricate, or the geometry impossible for a machine tool to reach.
| Conventional | Non-conventional | |
| Removes material by | Physical cutting tool | Thermal, electrical, or abrasive energy |
| Tool contact | Direct cutting force | Little or none |
| Best for | Standard shapes, most metals, speed | Very hard or delicate stock, intricate features |
| Examples | Turning, milling, drilling, grinding | EDM, laser, water jet |
Conventional Machining Operations
1. Turning
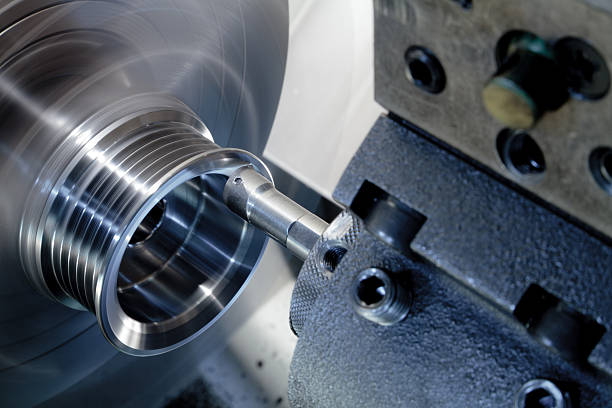
The turning process removes material from a rotating workpiece using a stationary single point cutting tool. The workpiece rotates on a lathe while the cutting tool remains stationary, cutting cylindrical parts, external threads, grooves, and internal bores.
It runs on manual lathes or CNC turning centers. It suits aluminium, steel, stainless steel, titanium, brass, and high temperature alloys. Typical uses are shafts, bushings, threaded rods, and precise cylindrical components. CNC turning delivers smooth, round surfaces with high precision.
2. Milling
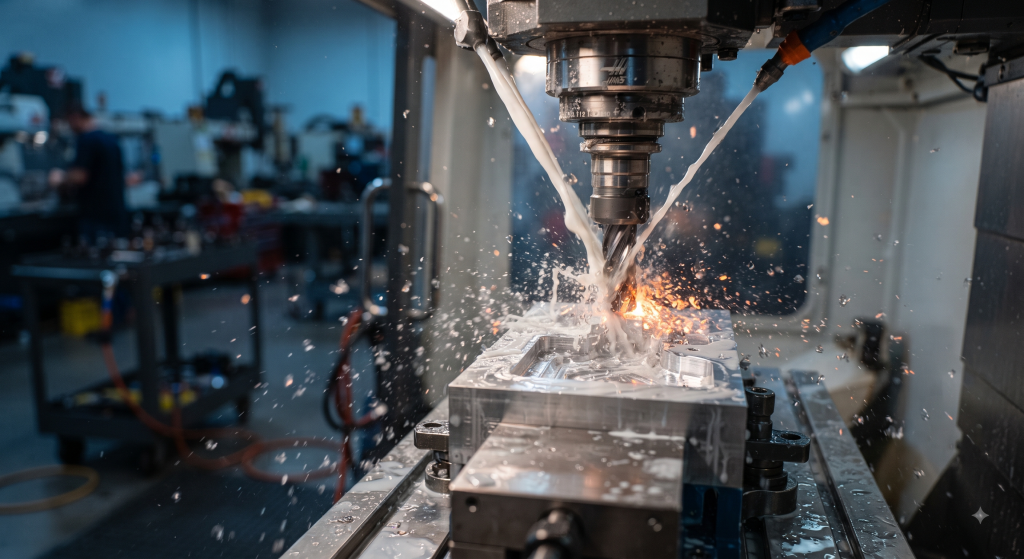
CNC Milling uses rotary cutters with multi point cutting tools to remove material from a stationary workpiece. Because the cutter moves across multiple axes, milling operations produce flat surfaces, slots, pockets, contours, and complex shapes.
On CNC milling machines, computer-aided design drives tool paths to hold tight tolerances. Common operations include face milling, end milling, slot milling, and chamfer milling. Three-axis milling machines cover most parts. Four-axis and five-axis milling machines handle complex geometries in a single setup.
3. Drilling
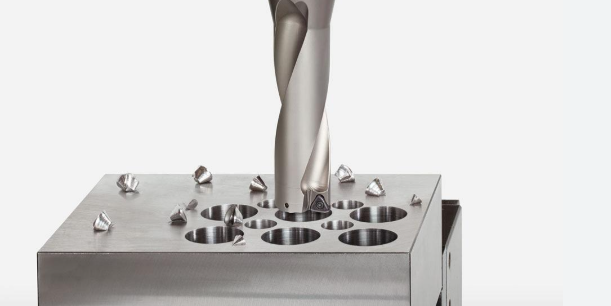
Drilling operations produce cylindrical holes with a rotating drill bit fed along its axis. Drilling creates blind holes or through holes, with quality set by the drill bit, cutting speed, and feed rate.
Drilling works on almost any metal, including soft metals and hard alloys. Peck drilling clears chips on deep bores. Gun drilling keeps deep holes straight.
4. Boring
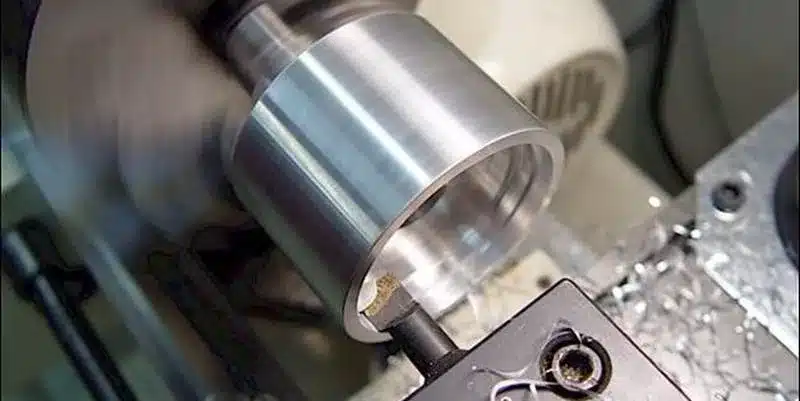
Boring is a precision machining process that enlarges and refines an existing hole using single point boring tools, improving diameter and positional accuracy. It brings a drilled hole to precise dimensions, makes it truly round, and aligns it to a datum. Its material removal rate is kept relatively low, which allows light finishing passes and helps maintain tight tolerances.
It runs on lathes, CNC mills, and boring mills. Unlike reaming, boring corrects hole position and roundness. It is common for engine cylinders and bearing bores.
5. Reaming
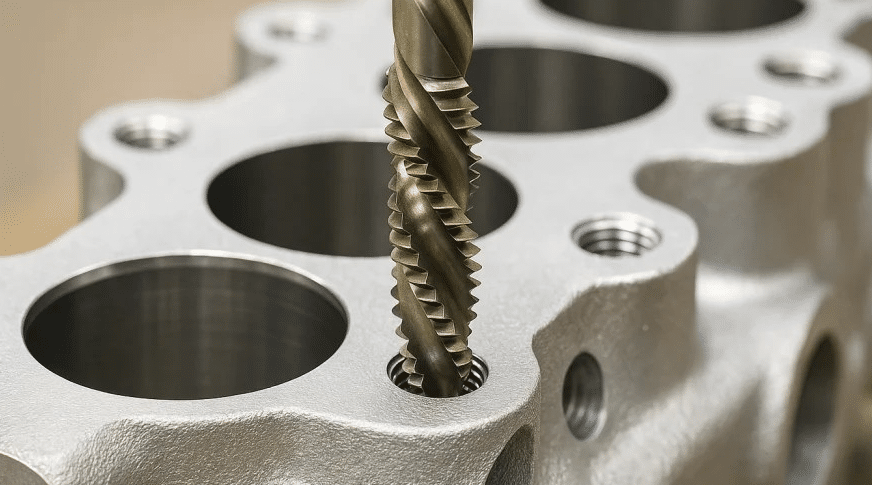
Reaming is a secondary finishing process that refines an existing hole. It removes a thin layer to improve accuracy and smoothness. It refines a hole already made by drilling or boring rather than creating a new one.
Different tasks use hand, machine, shell, or taper reamers. Reaming is essential for aerospace components, medical tools, and automotive parts where bores need precise sizing for press fits.
6. Tapping
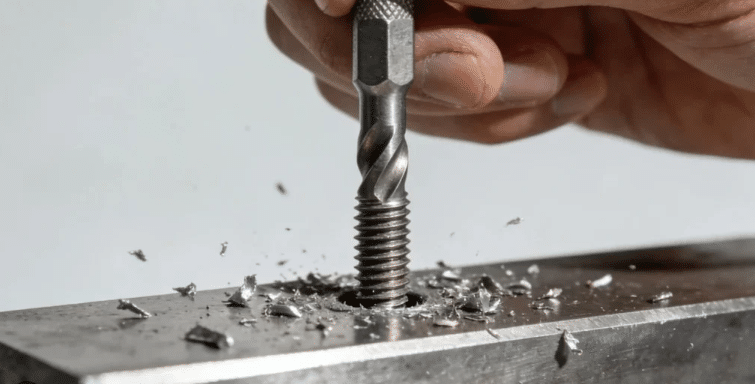
Tapping cuts internal threads inside a hole using a tap, allowing the part to accept bolts and screws. As the tap advances, its cutting edges form the thread profile.
Hand taps suit manual work. Machine taps run on a drill press or CNC machine. Forming taps displace rather than cut metal. Correct selection and lubrication prevent tool wear, broken taps, and stripped threads.
7. Grinding
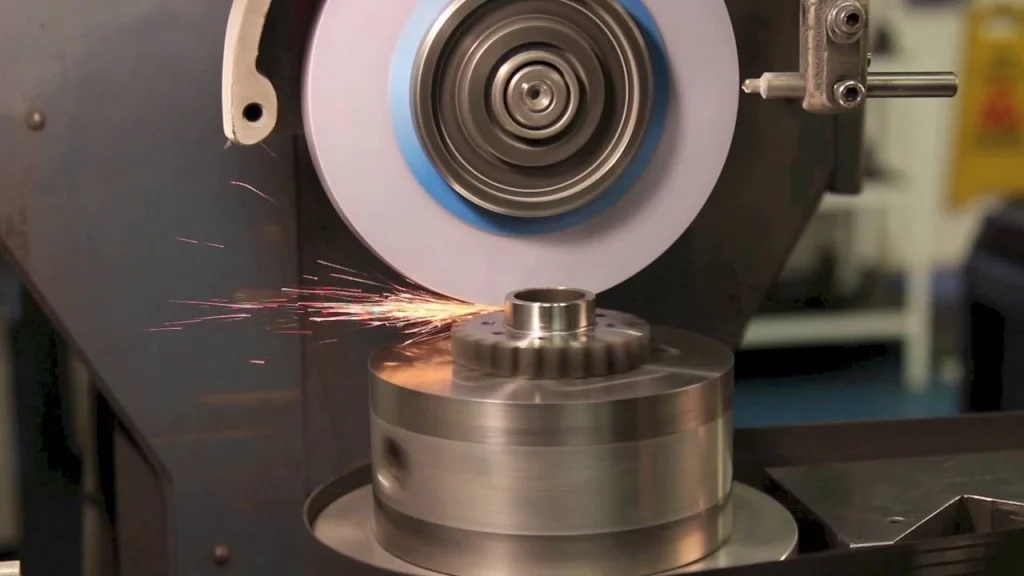
Grinding removes small amounts of material with a rotating abrasive wheel made from abrasive material. The fine abrasive particles on the wheel act as tiny cutting edges. As abrasive particles dull, they break away and expose fresh ones, making the wheel self-sharpening.
It handles very hard metals and delivers a fine surface finish, commonly Ra 0.2 to 0.8 µm. Surface grinders handle flat faces, while cylindrical grinders handle outer diameters. Grinding works well on hardened steel, ceramics, and brittle materials.
8. Planing
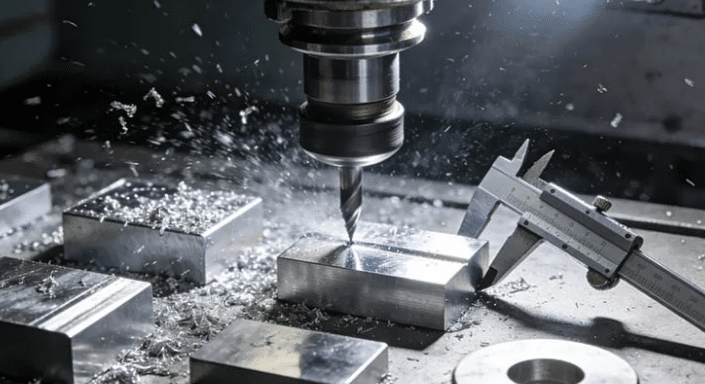
Planing produces large flat surfaces and straight slots. The workpiece moves back and forth beneath a stationary cutting tool, cutting in linear strokes. The tool remains stationary while the table translates. Shaping is similar, but the cutting tool moves while the workpiece stays fixed.
Planing suits large, rigid components beyond milling capacity, such as machine bases and long guideways.
9. Broaching
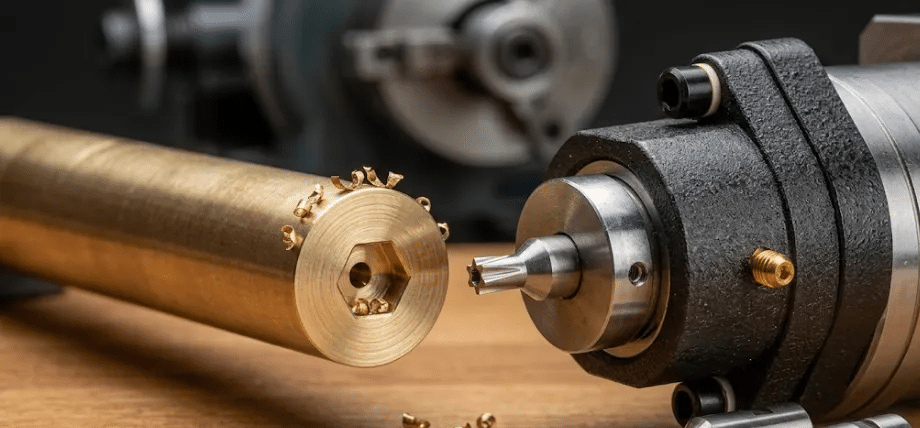
Broaching pushes or pulls a long, toothed broach through the workpiece. Each tooth sits slightly higher than the last, so the full profile is cut in one pass.
Internal broaching produces keyways and splines. External broaching shapes flat surfaces and gear teeth. It holds tolerances near ±0.005 mm, making it common in volume automotive production.
10. Knurling
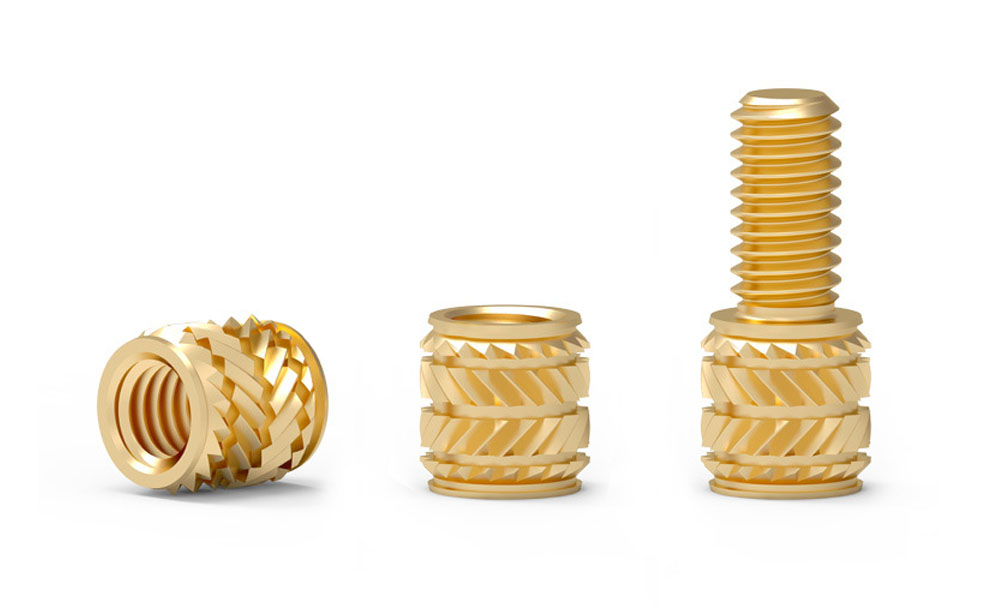
Knurling creates a textured pattern on a workpiece’s surface layer, usually by displacing metal rather than cutting it. It improves grip, appearance, and press-fit preparation.
Hand knurling suits softer materials. Machine knurling on a lathe gives finer patterns in harder metals. Common uses include tool handles, mechanical pencils, and control knobs.
Non-Conventional Machining Process
These techniques exist for jobs conventional cutting cannot do: stock too hard, walls too thin, cavities too deep, or features too intricate for any machine tool.
11. Electrical Discharge Machining (EDM)
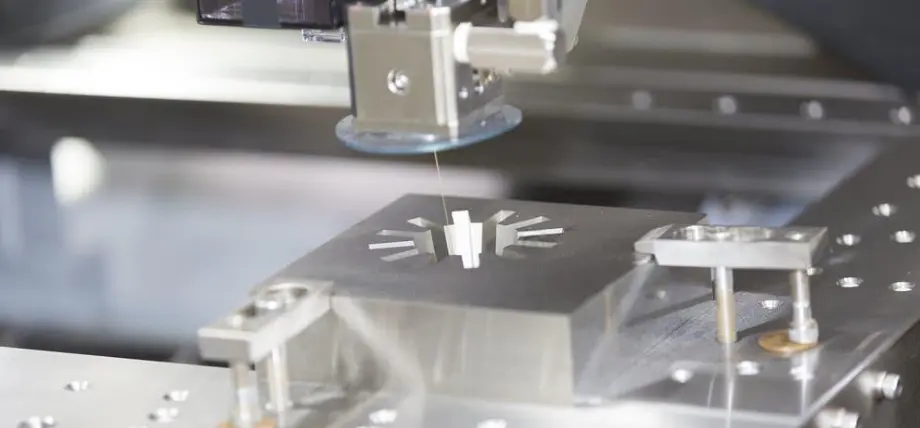
EDM is a thermal processing method that removes material with controlled electrical sparks rather than mechanical force. Each spark melts and vaporizes a tiny amount of metal, with dielectric fluid flushing the debris. With no cutting force, it handles very hard or delicate metal parts.
It works only on conductive metals but produces complex shapes, deep cavities, and sharp internal corners at high precision (about ±0.005 mm). The three variants are die-sinking, wire, and hole-drilling EDM. It dominates mold, die, and tooling work.
12. Laser Beam Machining
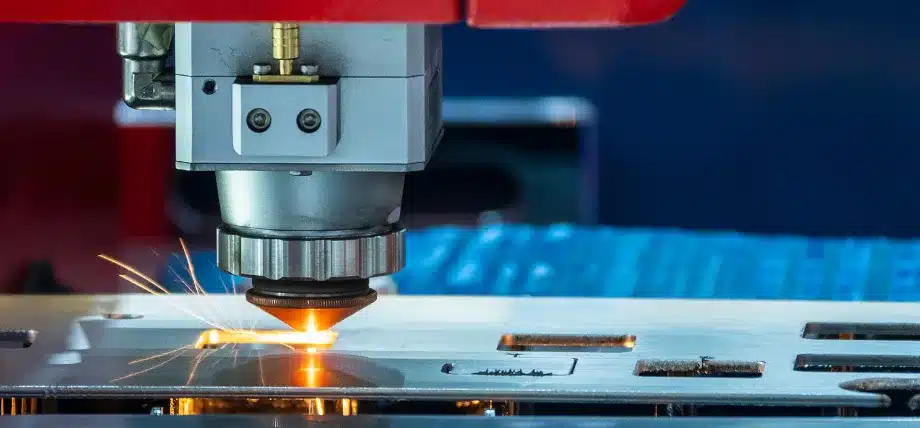
Laser beam machining is another thermal processing technique that focuses a high-energy beam to melt, burn, or vaporize material along a programmed path. It cuts intricate profiles with a very narrow kerf and no tool wear or mechanical stress.
Fiber and CO2 lasers cut, engrave, and create holes in many metals and other materials, excelling at fine detail and thin sheet. The heat-affected zone and reflectivity of copper and aluminum are the main considerations. Laser machining is common in electronics, medical devices, and precision sheet work.
13. Water Jet Cutting
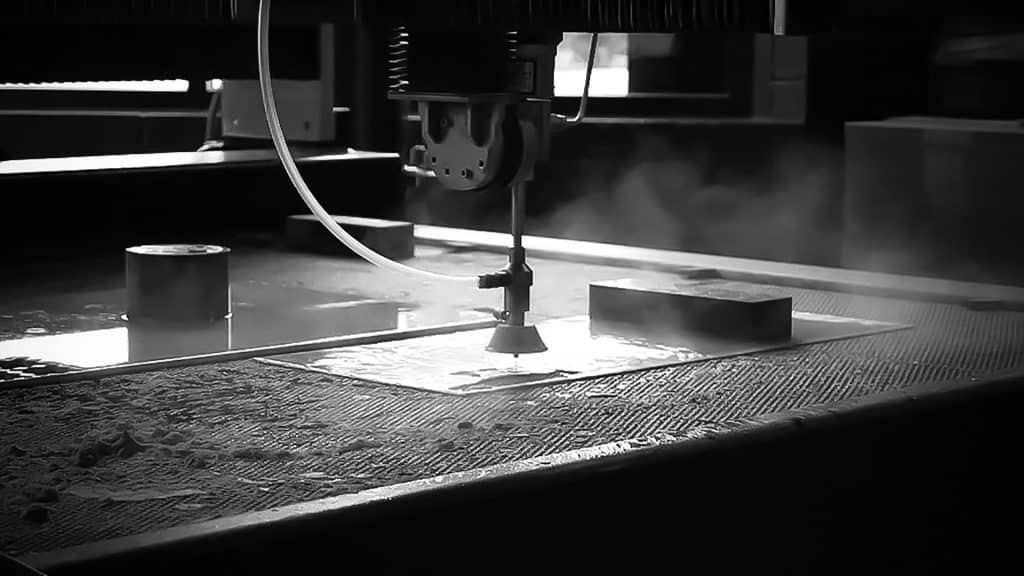
Water jet cutting uses an ultra-high-pressure water stream, often mixed with abrasive, to erode material. Pumps typically run near 60,000 psi and reach 90,000 psi. Cutting is cold, so there is no heat-affected zone and no warping or discoloration.
It cuts many different materials, including metal, stone, glass, composites, and thick plate, and suits heat-sensitive stock. It is also effective for machining softer materials without crushing or deforming them. Typical uses include thick-plate cutting, gaskets, and complex parts needing a clean, stress-free edge.
14. Other Machining Processes
Beyond the primary thermal and mechanical cutting methods, several specialized non-conventional processes handle extreme material or precision requirements.
- Chemical machining process
- Abrasive jet machining
- Plasma arc machining
- Ultrasonic machining
- Electrochemical machining
- Ion beam machining
Machining Processes Compared
The typical tolerances below are industry values, typically ranging with the machine, metal, and setup.
| Process | Category | Removes material by | Typical tolerance | Best suited for |
| Turning | Conventional | Single-point tool, rotating part | ±0.025 mm | Cylindrical shafts, threads |
| Milling | Conventional | Rotary cutters, multiple edges | ±0.025 mm | Flat faces, slots, complex shapes |
| Drilling | Conventional | Rotating drill bit | ±0.05 mm | Round holes, bolt patterns |
| Boring | Conventional | Single-point tool enlarging a hole | ±0.01 mm | Precise, true, aligned bores |
| Reaming | Conventional | Rotary reamer finishing a hole | ±0.01 mm | Smooth, accurate finished holes |
| Tapping | Conventional | Tap forming threads | Thread class | Internal threads for fasteners |
| Grinding | Conventional | Abrasive wheel | ±0.005 mm | Hard metals, fine surface finish |
| Planing | Conventional | Single-point tool, linear stroke | ±0.05 mm | Large flat surfaces, guideways |
| Broaching | Conventional | Multi-tooth broach, one pass | ±0.005 mm | Keyways, splines, gear teeth |
| Knurling | Conventional | Displacing surface metal | Pattern-based | Grips, textures, press-fit prep |
| EDM | Non-conventional | Electrical spark erosion | ±0.005 mm | Hard conductive metals, molds, dies |
| Laser | Non-conventional | Focused thermal energy | ±0.02 mm | Intricate profiles, thin sheet |
| Water jet | Non-conventional | High-pressure water and abrasive | ±0.1 mm | Thick plate, heat-sensitive metals |
How to Choose the Right Machining Process
Work through these five factors in order and the field narrows quickly.
Material
Free-machining metals like aluminum and brass suit almost any conventional process. Hardened steels point to grinding, hard turning, or EDM. Brittle or hard metal alloys often suit it. Heat-sensitive stock favors a water jet, which cuts cold.
Geometry
External cylindrical features suit turning; flat faces and slots suit milling; internal profiles suit broaching or wire EDM; deep cavities suit EDM or laser.
Tolerance and finish
Looser than ±0.05 mm is easy for milling and turning. Tighter than ±0.025 mm needs grinding, honing, or EDM. Surfaces below Ra 0.8 µm need a dedicated finishing operation.
Volume
Low volumes favor flexible CNC milling and CNC turning. High volumes reward dedicated processes like broaching or dedicated form tooling. Medium volumes suit multi-operation CNC machining centers.
Cost
Specialized processes like EDM carry high equipment costs and are justified only when no cheaper option exists. For most machined parts, standard CNC machining gives the best cost per part, and competitive pricing from an outside machine shop often beats buying capacity you rarely use.
Which Industries Rely on Machining?
Metal machining underpins manufacturing in every sector where accuracy is non-negotiable.
- Aerospace machines airframe and engine components from titanium and aluminum.
- Automotive machines engine blocks and transmission components at production volume. Medical machines implants and instruments from titanium and 316L stainless.
- Electronics machines heat sinks and enclosures.
- Oil and gas machines valve bodies and downhole tools. In each case, the metal machining process is chosen to hit the required dimensions, surface finish, and volume.
Frequently Asked Questions
What are the types of CNC machining processes?
They split into conventional machining operations that use a cutting tool (turning, milling, drilling, boring, reaming, tapping, grinding, planing, broaching, knurling) and non-conventional metal machining processes that use energy (EDM, laser, water jet cutting).
What are the three main types of CNC machining?
The three main types are traditional (conventional) machining, non-traditional machining, and CNC machining, which controls both digitally. Some sources instead cite turning, milling, and drilling as the three basic types.
Which machining process is the most accurate?
Grinding, EDM, and honing hold the tightest tolerances, around ±0.005 mm and finer, with the wheel giving the best surface finish.
Is machining a subtractive or additive process?
Machining is subtractive manufacturing: it removes excess material from a solid block, the opposite of 3D printing, which builds parts up layer by layer.
How do I choose the right machining process?
Consider the raw material, the geometry, the tolerance and surface finish, the production volume, and the equipment cost, in that order.
