

 EU
Two parts can come off the same machine, cut from the same material, and still turn out differently. One has a clean surface and holds its dimensions. The other shows chatter marks, or the tool wears out halfway through the run. Often the difference traces back to a single geometry choice on the cutting tool: the rake angle, the angle between the tool’s rake face and a reference plane perpendicular to the cutting direction. This angle helps determine how the tool meets the material, which directly affects cutting force, heat generation, vibration, surface finish, tool life, and overall machining efficiency. This guide explains what rake angles are, the main types, how they vary by material and application, and how to choose the right one to improve part quality, tool durability, and production results.
What Is Rake Angle?
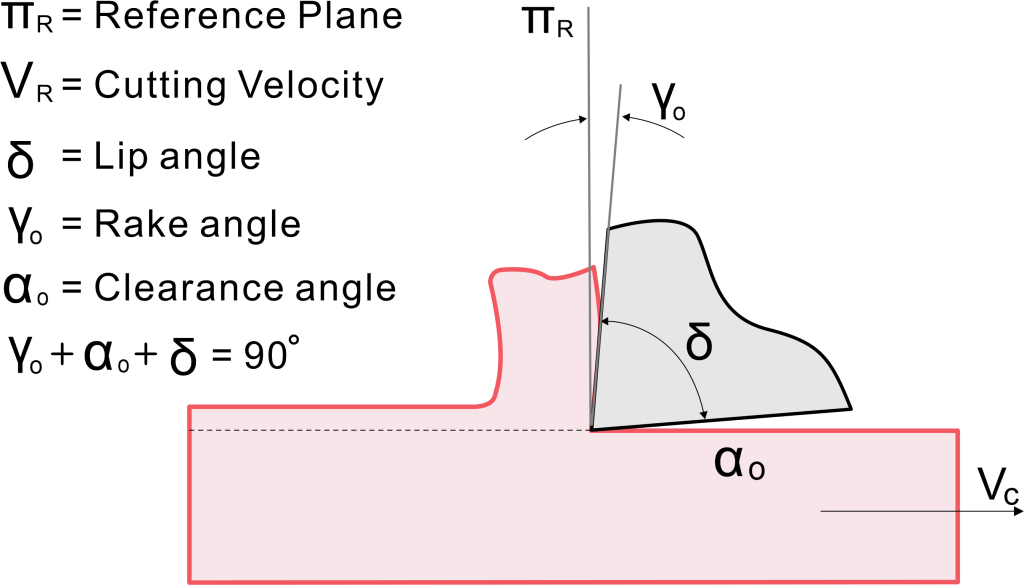
The rake angle is the angle between the rake face of a cutting tool and the reference plane perpendicular to the cutting direction. The rake face is the tool’s cutting face, or rake surface, and it is the surface the chip slides across as it separates from the workpiece. This single angle decides how the tool meets the material. The cutting tool rake angle also influences cutting mechanics and chip formation during the cutting process. A tool can slice into the workpiece cleanly, or it can push and shear the material aside. The difference between those two actions comes down to a few degrees of geometry.
Rake angle is measured in degrees, and it can be positive, negative, or zero. Each setup changes how the cutting edge behaves under load, how much heat builds up, and how long the tool lasts before it needs replacing.
Types of Rake Angle
Positive Rake Angle
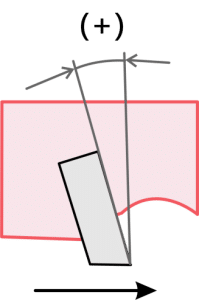
The tool face slopes away from the cutting edge, back into the body of the tool. This creates a sharp, thin edge that slices into the material rather than pushing it aside. Positive rake works well on softer, more ductile materials such as aluminium and low-carbon steel, especially for cutting ductile materials because it reduces chip adhesion where cutting force and heat control matter more than raw edge strength.
Advantages:
- Lower cutting force. The sharp edge shears into the material instead of pushing it aside, so the spindle works less to remove the same amount of stock.
- Reduced heat generation. Less friction between chip and tool face means less heat transfers into the cutting zone, which helps protect both the tool and the workpiece surface while improving overall cutting tool rake performance.
- Better chip evacuation on gummy or soft materials. The steep face angle guides chips away from the cut, improving smoother chip control and chip flow along the tool bit rather than letting them curl back and re-cut.
- Smoother surface finish on many alloys. Cleaner shearing action leaves fewer torn or dragged surface marks than a blunter edge would, especially when the tool rake angle is matched to the material.
Disadvantages:
- Weaker edge, prone to chipping on hard or interrupted cuts. There is less material behind the edge to absorb sudden impact, so it fails faster under shock loads.
- Not suited to high-impact or heavy roughing operations. The thin geometry that helps with soft materials becomes a liability once cutting forces or interruptions increase.
Negative Rake Angle
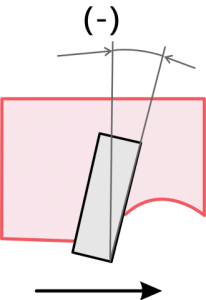
The tool face slopes the opposite way, thickening the edge and pushing the cutting action further from the workpiece. A negative rake angle tool is typically chosen when edge strength matters more than cutting ease. This geometry resists chipping under heavy or interrupted loads, which makes it a common choice for hard, brittle materials like cast iron and titanium alloys.
Advantages:
- Stronger, more durable edge. The thicker wedge behind the cutting edge spreads load over more material, so the edge holds up longer under stress.
- Better resistance to chipping and fracture. Sudden shocks from interrupted cuts are absorbed rather than concentrated on a thin, fragile tip.
- Handles interrupted cuts and hard materials more reliably. The extra mass behind the edge tolerates the repeated impact that comes with holes, slots, or scale on the surface.
Disadvantages:
- Higher cutting forces. This rake angle tool takes more energy to push through the material, increasing spindle load compared with freer-cutting geometries and loading the workpiece more heavily.
- More heat generated at the tool tip. Increased friction from the blunter geometry raises temperatures at the cutting zone, which can accelerate wear if not managed with coolant or coating.
- Can leave a rougher surface finish if not paired with the right speeds and feeds. The less efficient shearing action can tear the surface rather than cut it cleanly unless parameters are tuned to compensate.
Zero Rake Angle
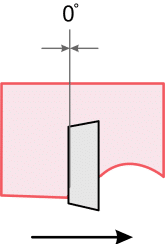
The tool face sits perpendicular to the feed direction, with no slope in either direction. It is a compromise geometry, simpler to grind and often used as a starting point before a shop settles on a positive or negative setup for a specific job.
This orientation is also common in general turning when a shop wants balanced performance.
Advantages:
- Simple geometry, easier and cheaper to manufacture and regrind. A flat, perpendicular face needs less precision to produce than an angled one, which keeps tooling costs down.
- Predictable, balanced performance across a range of materials. Without a strong bias toward force reduction or edge strength, it behaves consistently across varied jobs.
Disadvantages:
- Rarely optimal for either force reduction or edge strength. It gives up some of the benefits of both positive and negative rake without matching either at its best.
- Tends to be a middle-ground choice rather than a first pick for demanding applications. Once a job calls for maximum efficiency or maximum durability, a purpose-chosen angle usually outperforms it.
Why Rake Angle Is important in Machining
Rake angle looks like a small detail on a technical drawing, but it affects three things engineers care about on every job: cutting force, tool life, and surface finish.
Cutting Force
A higher positive rake angle reduces the force needed to cut. The tool bites into the material at a sharper angle, so less energy goes into deforming the workpiece before the chip separates, which improves chip flow and can lower cutting temperature. This matters on machines with limited spindle power, and it matters when machining thin-walled or flexible parts that can deflect under heavy cutting loads.
Better chip control can also improve machining performance on low-power setups.
Tool Life
A stronger negative rake angle does the opposite job. It thickens the wedge angle of material behind the cutting edge, which improves tool strength by spreading the load over a larger cross-section. On hard or interrupted cuts, that extra mass protects the edge from chipping or fracturing. The trade-off is higher cutting force and more heat, and potentially faster tool wear if the geometry is too aggressive for the material.
Heat and Finish
Rake angle also governs how much friction builds up between the chip and the tool face, influencing chip formation as material moves across the cutting edge. Too little rake can hurt chip control, raising friction, temperature, and surface roughness, while a freer-cutting angle often produces thinner, curled chips. Too much rake on the wrong material, and the edge weakens faster than it should. Getting the angle right keeps heat manageable and helps produce a cleaner, more consistent surface.
Vibration and Stability
Rake angle also affects how stable a cut feels. A very positive angle can pull the tool into the material, which helps on light finishing passes but can encourage chatter on long, unsupported cuts. A negative or neutral angle pushes back against the workpiece instead, and a neutral rake is perpendicular to the feed direction, which can dampen vibration on heavier roughing passes, provided the machine is rigid enough to handle the extra force. Shops fighting chatter on thin or overhanging parts often find rake angle worth adjusting alongside speeds and feeds. If chip evacuation is poor, neutral geometry can also increase power consumption.
The relationship between rake angle and edge strength is easiest to see side by side. A positive angle creates a thin, sharp wedge that cuts easily but has less material behind it to absorb shock. A negative angle creates a thick, blunt wedge that resists chipping but requires more force to push through the material. Most tooling decisions sit somewhere between these two extremes, depending on the material and the machine.
Rake Angles for Different Materials
Different materials respond differently to the same rake angle, so tooling recommendations vary by workpiece.
Aluminium and soft non-ferrous metals. These materials are soft and ductile, and they tend to build up on the cutting edge if the angle is too shallow. A positive rake angle, often in the range of 15 to 20 degrees , helps the tool shear through the material cleanly and clear chips before they weld to the tool face.
Mild steel and carbon steel. These materials sit in the middle of the hardness range. A moderate positive rake, often around 5 to 10 degrees , balances cutting force against edge durability.
Stainless steel. Stainless work-hardens quickly, which makes edge sharpness and consistent rake geometry important. A slightly positive rake angle is common, paired with sharp, well-maintained edges to avoid excessive heat build-up during the cut.
Cast iron. Cast iron is hard and abrasive, and it produces short, brittle chips. A neutral to negative rake angle suits this material, since edge strength matters more than shear efficiency here.
In specialty applications such as cutting cortical bone, a rake angle of 20–35° can be favorable.
Exact angle recommendations depend on the tool material, coating, and cutting conditions, so treat the ranges above and other recommended rake angles as starting points rather than fixed rules.
How Do You Choose the Right Rake Angle for Your Project?
Selecting a rake angle is not a single decision. It depends on the material, the cutting conditions, and the machine doing the work.
Match Based on Material Hardness and Properties
Choosing the correct rake angle starts with the material’s hardness, ductility, and tendency to form chips. Softer, more ductile materials generally pair well with positive rake angles, since the priority is reducing force and controlling heat. Harder, more brittle materials favour negative or neutral rake angles, since the priority shifts to protecting the edge from fracture. Start with the material’s known machining characteristics, then adjust from there based on results. Some form tools often come with pre-set insert geometry suited to specific materials.
Adjust Based on Machining Conditions
Continuous cutting, where the tool stays engaged with the material throughout the pass, allows for more aggressive positive rake angles because the edge is not repeatedly shocked by entry and exit.
Interrupted cutting, such as machining a surface with holes or slots, puts repeated impact stress on the cutting edge. In these conditions, a less positive or negative rake angle holds up better, since the thicker edge resists the repeated shock of entering and leaving the cut.
Match With Machine Tool Capabilities
Rake angle choices also depend on what the machine can support, since the effective rake angle can shift with holder setup and tool position rather than staying fixed at the nominal insert value. Lower-power spindles benefit from positive rake angles that reduce cutting force. Older or less rigid machines may struggle with the higher forces generated by negative rake tooling, which can lead to vibration or chatter. Matching tool geometry to the machine’s rigidity and power output is as important as matching it to the material.
Milling cutters can show a different effective rake depending on the cutter body and setup.
Consider Tool Material and Coating
The rake angle does not work in isolation from the rest of the tool, and the effective rake seen at the cut also depends on insert seating and holder geometry. The selected insert geometry should match both the tool material and the intended cutting conditions. Carbide, ceramic, and coated tools each tolerate different stresses, and a coating such as TiAlN or TiN can offset some of the heat and friction that a less favourable rake angle would otherwise create. A slightly conservative rake angle paired with the right coating can sometimes outperform a more aggressive angle on an uncoated tool.
Factor in Production Volume and Tool Cost
A single prototype run can tolerate a less efficient rake angle if it still gets the part made. A high-volume production job cannot. Small gains in cutting force or tool life add up quickly across thousands of parts, so it is worth spending more time optimising rake angle, and possibly more on tooling, once a job moves from one-off to repeat production.
Test and Adjust Based on Wear Patterns
The angle that looks right on paper does not always perform best in practice. Watching how a tool wears, whether it chips at the edge, builds up heat discolouration, or wears evenly, gives a clearer picture than theory alone. Shops that track wear patterns across jobs tend to refine their rake angle choices faster than those relying on general guidelines.
Conclusion
Rake angle is not merely a theoretical angle on a cutting tool. It is a practical lever that engineers use every day to balance machining efficiency, surface quality, and tool life. Getting it right on paper is one thing, but getting it right in production, across different batches, machines, and tolerances, takes experience.
If you are working through tool geometry decisions for an upcoming production run, it is worth paying closer attention to how rake angle interacts with your specific materials and machines before committing to a full batch. Aria Manufacturing’s engineering team works with these tooling trade-offs regularly across a range of materials and production volumes, and you can consult with Aria to optimise your specific CNC machining processes and ensure reliable production outcomes.
